Manufacturers evaluating this process juggle several variables at once: fastener strength, dimensional consistency, material usage, production volume, assembly complexity, and tooling investment. Get the balance wrong, and you end up with expensive tooling that doesn't pay for itself, or a part that fails under load.
This article covers how cold heading works, common forming methods, where it beats machining, where it doesn't, and what you need to gather before requesting tooling for your own project.
Key Takeaways
- Cold heading shapes metal through controlled material flow, primarily upsetting and extrusion.
- Near-net-shape cold heading cuts material waste and reduces secondary operations.
- One cold-headed part can replace a multi-piece assembly when geometry and volume support it.
- Review design, material, tolerances, tooling progression, and supplier capability together before you commit.
What Are Cold-Headed Fasteners and Assemblies?
Defining the Process
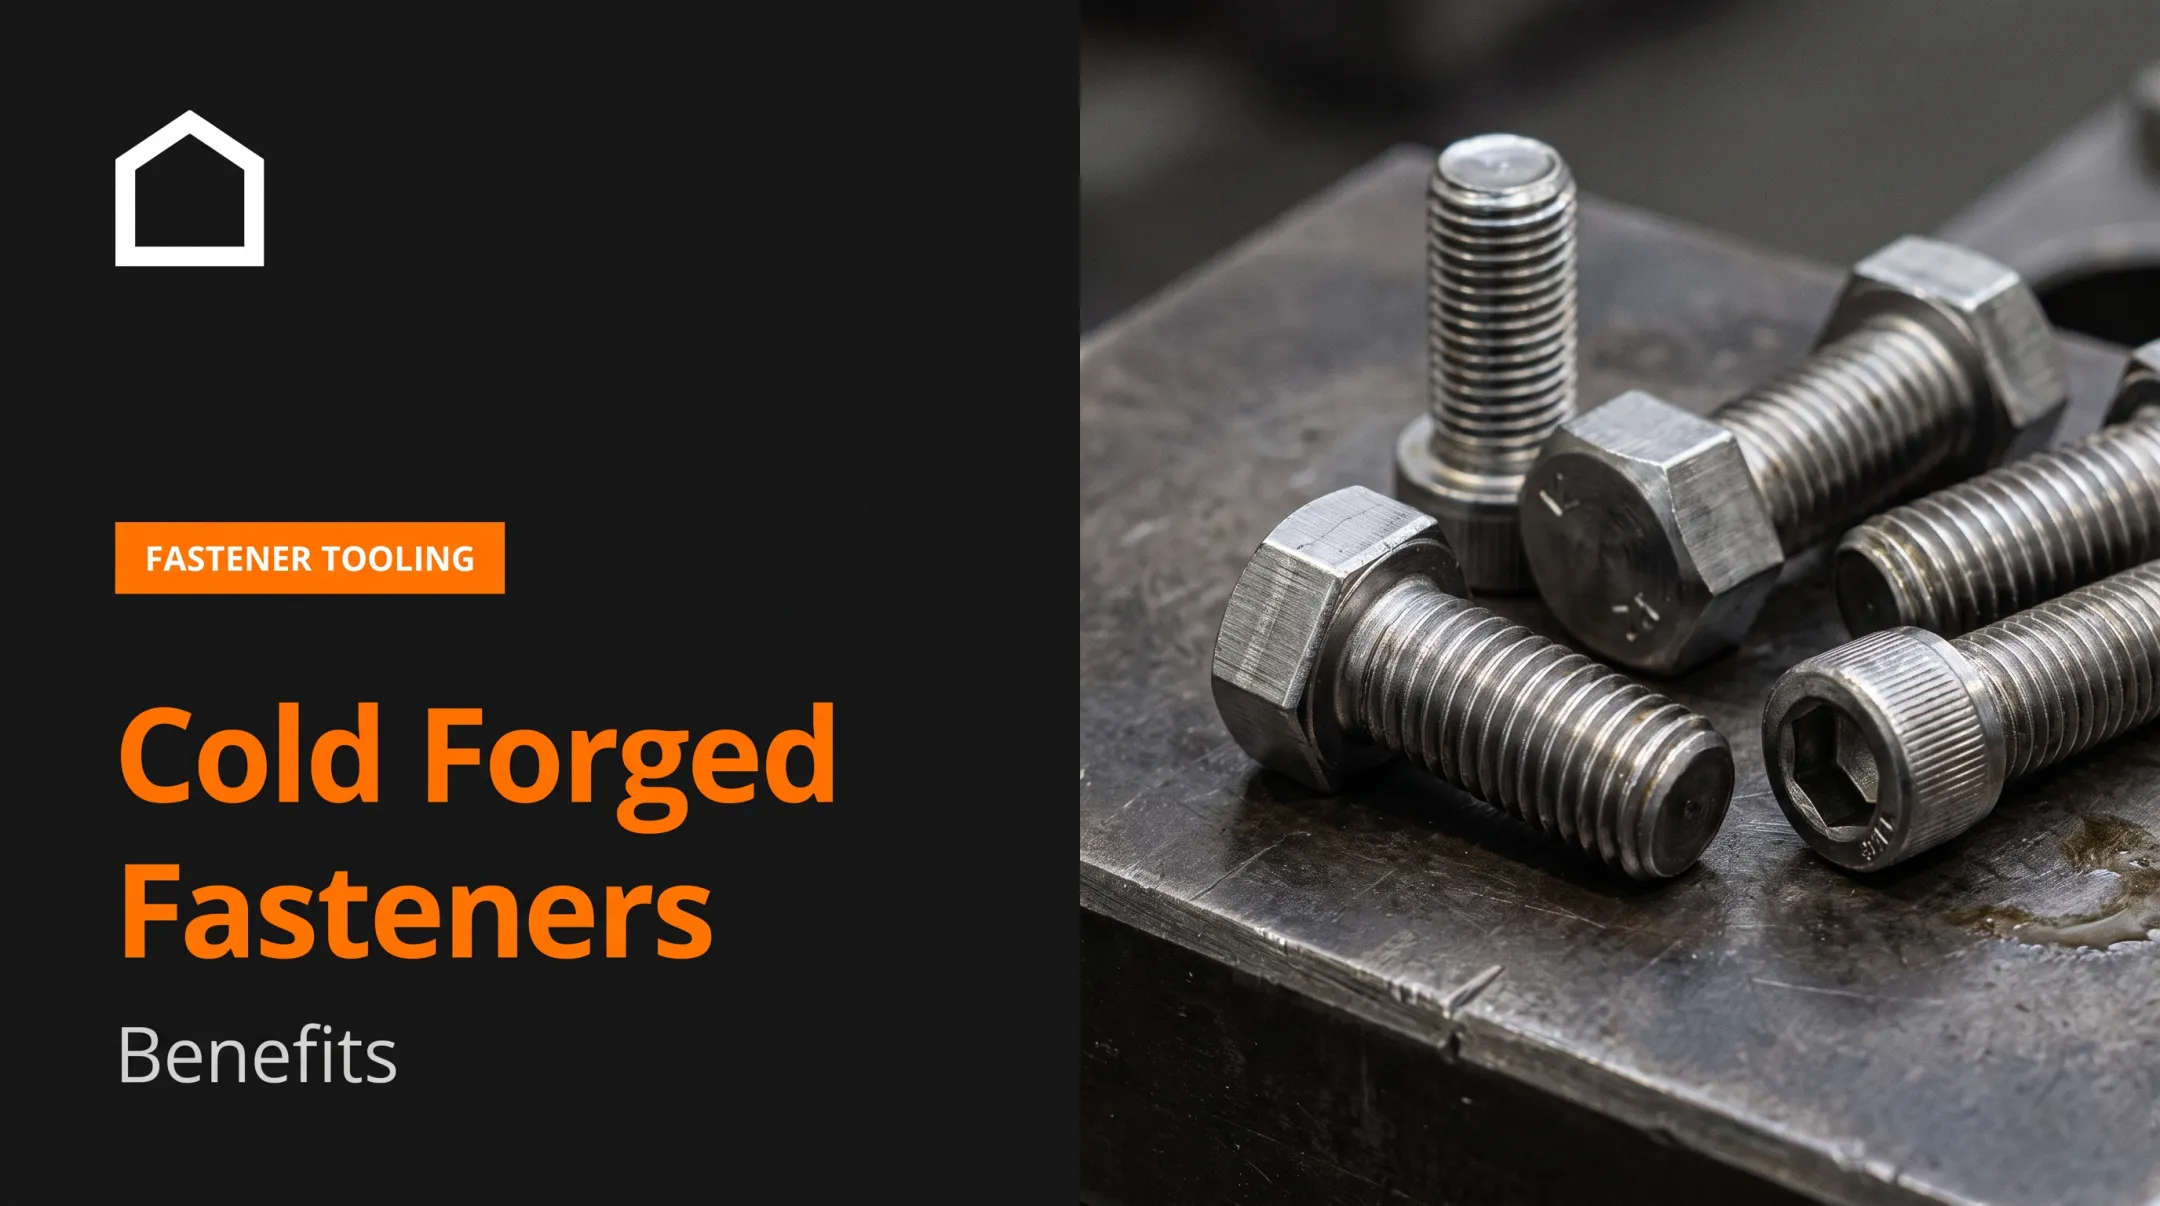
A cold-headed fastener is any bolt, screw, rivet, stud, pin, or specialty component formed by moving wire or a blank through dies and punches without intentional heating. "Cold" refers to the forming temperature, not the finished part's condition.
Cold forming is the umbrella category : any room-temperature metal displacement process. Cold heading is the fastener-focused subset, most often used to create heads via upsetting. In that framing, cold forming covers extrusion and general component shaping; cold heading focuses on the head-forming step.
The Assembly Connection
Cold heading can build multiple features into one component:
- Heads, shoulders, flanges, and shanks in a single forming pass
- Internal cavities via backward extrusion
- Integrated recesses that eliminate a separate joining step
A cold-headed part might be one piece within a larger assembly, or it might replace an entire multi-piece subassembly if the function can be formed rather than joined. That call depends on load requirements and whether the geometry can be formed as one piece.
How the Cold Heading Process Works
Blank Preparation
Wire is drawn or sized as needed, then sheared into slugs sized to match finished-part volume. Blank diameter, length, material condition, and cleanliness all affect how well the metal fills the die.
Dirty or inconsistent stock causes:
- Incomplete die filling
- Surface defects
- The need for extra forming stages to compensate
Progressive Tooling
A cold header moves each blank through a tooling progression that builds the shape in stages instead of one heavy blow. Typical stations include:
- Cut-off and transfer
- Die and punch forming
- Holders that control metal flow between blows
Nedschroef describes multi-station headers working several blanks at once: a finished part leaves the last die on every stroke as a new blank enters the first. Station counts usually fall between one and seven. Geometry and required reductions set the number for each job.

Forming Techniques
Upsetting shortens a section and pushes metal outward to form a head, flange, or shoulder.
Forward extrusion drives metal ahead through the die to narrow or lengthen a section.
Backward extrusion sends metal back around a punch to form holes or internal cavities.
Finishing and Quality Checks
Depending on the design, parts may need:
Trimming or piercing to remove flash or open holes
Thread rolling
Heat treatment or plating
Grinding, shaving, or polishing
Secondary machining for features the header can't economically produce
Dimensional inspection, surface checks, and mechanical testing where specified
Consistent output also depends on ongoing tooling maintenance. Skip that step and tolerances drift long before anyone notices on the shop floor.
Benefits and Limitations of Cold Heading
Material Efficiency and Economics
Forming material into a die displaces metal rather than cutting it away, so cold heading typically generates less scrap than machining.
A 2016 Medical Design Briefs case study found an optimized cold-heading progression ran 90-300 parts per minute versus 6-20 PPM for a comparable screw-machined design. The screw-machined part lost roughly half its mass to scrap. Results still depend on geometry and material, so treat that case as a benchmark rather than a guarantee.

Near-net-shape production generally reduces:
- Raw material consumption
- Machining time
- Handling and inspection steps
Performance and Design Benefits
Controlled material flow work-hardens the metal, which can improve strength and wear resistance. How much strength you gain depends on alloy, reduction ratio, grain flow, and any post-forming heat treatment.
Integrated features can also cut part count in some assemblies, reducing welding, brazing, or manual assembly steps. Validate load and service conditions before locking that design into production.
Limitations and Process Comparisons
Those gains come with trade-offs in tooling cost, shape flexibility, and volume fit. The table below compares cold heading with machining and hot heading:
| Factor | Cold Heading | Machining | Hot Heading |
|---|---|---|---|
| Temperature | Room temp | No bulk heat needed | ~1000°F to 2300°F |
| Tooling cost | High upfront | Lower dedicated cost | Lowest tooling cost |
| Shape flexibility | Limited by die design | Highly flexible | Broadest size range |
| Tolerances | Tight | Tight | Looser |
| Best fit | High volume | Low volume / complex geometry | Very large parts |
A historical trade report cited cold-forming tool sets running $5,000-$25,000, and low quantities often do not justify that spend. Use the range as a directional figure only, then confirm current tooling cost and expected die life with your supplier.

Materials, Tooling, Applications, and Quality
Material Selection
Commonly cold-headed materials include:
- Carbon and alloy steels
- Stainless steels
- Aluminum
- Brass and copper
- Other ductile, formable alloys
Feasibility hinges on ductility, work-hardening behavior, and whether the metal stays below fracture strength through every planned reduction. Push an alloy too far in one station and you get cracking instead of a formed head.
Tooling and Quality Requirements
Dimensional accuracy and tool life depend on several factors:
- Die and punch design
- Tool steel selection
- Alignment and lubrication
- Maintenance schedules
Quality FORM Tools works with tool steels including M2, D2, H13, and S5, each matched to different wear, toughness, and thermal stability needs.

Inspection and documentation requirements should match the customer's industry. A fastener for a pressure vessel needs a different quality trail than a generic wire form.
Applications and Part Suitability
Cold-headed parts are used across:
- Fasteners (bolts, screws, studs)
- Rivets and pins
- Electrical and industrial hardware
- Equipment components
Suitability depends on part geometry, tolerances, material, load requirements, production quantity, and finishing needs.
Choosing Cold Heading and Sourcing Tooling
Evaluate the Project First
Before committing to cold heading, work through a checklist:
- Annual and batch quantities, and whether volume justifies dedicated tooling
- Part geometry, including head-to-shank proportions and thread or cavity details
- Material ductility and work-hardening behavior
- Tolerance and surface-finish requirements
- Expected loads in service
- Secondary operations needed after forming
- Tooling cost versus projected part volume
Compare cold heading against machining, hot heading, forging, stamping, or a hybrid approach. Cold heading isn't automatically the right call just because the part looks like a fastener.
Once the process fits, the next step is giving suppliers enough detail to quote accurately.
Prepare a Complete RFQ
A complete RFQ package includes:
- Current drawings or CAD models
- Material and heat-treatment specifications
- Tolerances, quantities, and delivery timing
- Sample parts, if available
- Inspection requirements and packaging expectations
- Details on existing heading or forming equipment
Be specific about whether you need finished fasteners, a new tooling progression, recess punches, dies, cut-offs, quills, feed rolls, or related production tooling.
With a clear package in hand, you can compare suppliers on capability—not just unit price.
Where Quality FORM Tools Fits In
Quality FORM Tools, based in Hammond, Indiana, supplies custom cold header tooling for manufacturers in fastener-forming, stamping, and forging. The cold header tooling line covers dies, punches, cut-offs, quills, feed rolls, wire draw dies, and complete die assemblies. Tools are built to print for new part numbers or replacement runs.
Its offerings include:
- Custom-made recess punches
- Complete cold heading tooling packages ready for production
- Replacement machine parts for stamping and forming presses
- Tooling built from M2, D2, H13, and S5 tool steels
Quality FORM Tools supports low-volume prototype work and high-volume production tooling through a domestic and overseas supplier network. For a new job or replacement components on existing equipment, submit prints and specs for a project-specific quote.
Frequently Asked Questions
What is a cold-headed fastener?
A fastener formed from wire or a blank at room temperature using dies and punches, rather than machined from solid stock. Common examples include screws, bolts, studs, rivets, and pins.
What is cold heading in manufacturing?
Cold heading is a forming process where wire or blanks move through progressive dies and punches, using upsetting or extrusion to build the final shape. No intentional heating is involved.
What are the key differences between hot heading and cold heading?
Cold heading runs at room temperature with higher forming force and tighter tolerances; hot heading uses elevated temperatures to lower flow stress, allowing broader shapes but looser tolerances. Hot heading also typically needs more secondary finishing.
Are cold-headed fasteners suitable for every assembly?
No. Suitability depends on material ductility, part geometry, load requirements, tolerances, production volume, and whether secondary operations are acceptable for your application.
How do I know whether cold heading or machining is right for my part?
Compare production volume, material usage, geometry complexity, tolerance requirements, tooling investment, and lead time. High-volume, ductile-material parts generally favor cold heading; low-volume or highly complex geometries often favor machining.